SOLID SILICONE COMPRESSION MOLDING SPECIALIST
HCR Compression Molding for Industrial Sealing Applications
High Consistency Rubber (HCR) compression molding is the engineered solution for large-format seals, thick-wall gaskets, and specialized compound applications where LSR injection molding becomes cost-prohibitive or technically unsuitable. ISO 13485 certified. 20 production lines. Shore A 20–90.
🔒 NDA signed immediately · Full material traceability on every batch · Certified compounds
When HCR Compression Molding Is the Right Choice
Not every silicone project needs LSR injection. For the right application, HCR compression molding delivers superior material versatility, lower tooling investment, and proven durability at industrial scale.
HCR compression molding is the preferred process for silicone components exceeding 150mm in any dimension, where LSR tooling costs become prohibitive for the required annual production volume.
HCR vs LSR: Choosing the Right Process
Both processes produce high-quality silicone components. The right choice depends on your part geometry, volume, and performance requirements.
| Feature | HCR Compression Molding | LSR Injection Molding |
|---|---|---|
| Best For | Large, thick-wall parts; Specialized compounds | Complex, micro-precision parts; High volume |
| Part Size | Up to 550mm × 550mm | Best below 200mm |
| Dimensional Tolerance | ±0.1mm to ±0.2mm | ±0.05mm |
| Tooling Investment | Lower initial cost | Higher (optimized for volume ROI) |
| Production Efficiency | Manual/Semi-automated | Fully automated 24/7 |
| Hardness Range | Shore A 20 – 90 | Shore A 5 – 80 |
| Special Compounds | Flame retardant / Conductive / Extreme heat | Standard medical/food-grade |
| Annual Volume | 1,000 – 50,000 pieces | 50,000 – 1,000,000+ pieces |
✅ Choose HCR when:
· Part size exceeds 150mm in any dimension
· Annual volume is below 50,000 pieces
· Flame retardant, conductive, or extreme-heat
compounds are required
· Initial tooling budget is the primary constraint
· Wall thickness above 5mm is required
⚡ Choose LSR when:
· Dimensional tolerance tighter than ±0.1mm is required
· Cleanroom production is mandatory
· Annual volume exceeds 100,000 pieces
· Part weight is below 50g
· Medical-grade biocompatibility is the primary requirement
Not Sure Which Process Fits Your Project?
Controlled HCR Manufacturing Workflow
Every compression molding batch follows a documented five-stage process to ensure dimensional consistency, hardness stability, and full material traceability.
01
HCR compound precisely weighed and pre-formed. Weight tolerance controlled to ±2% to prevent flash and short shots.
02
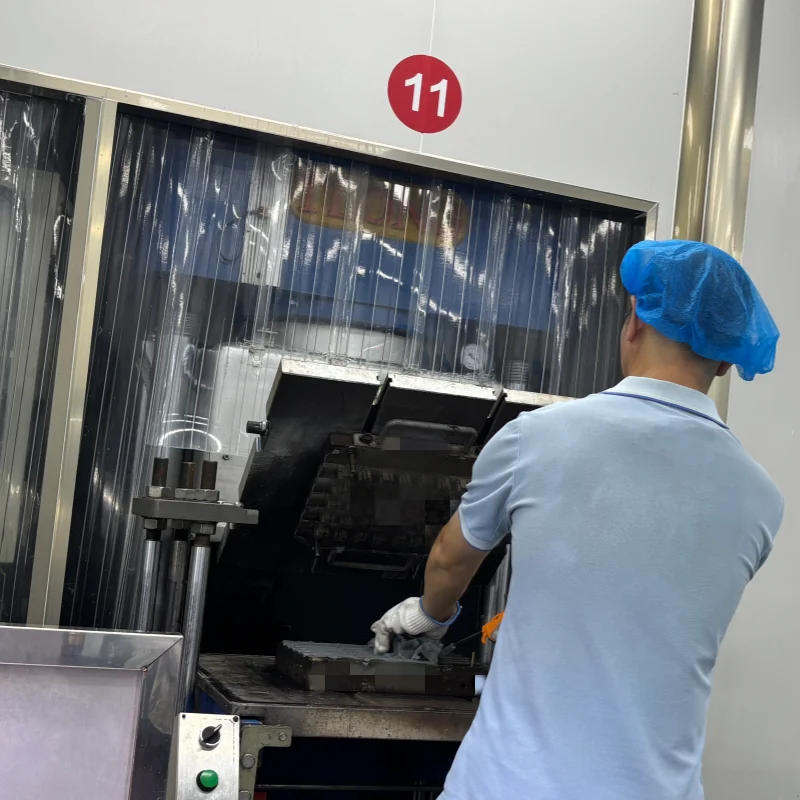
20 vulcanizing presses apply controlled heat and pressure. Daily output exceeds 30,000 components.
03
Cryogenic technology removes flash without dimensional distortion. Maintains edge integrity on complex profiles.
04
Every batch tested against Shore A specification. Deviation beyond ±3 Shore A triggers batch investigation.
05
Full dimensional OQC report with batch number, material lot, and cure parameters traceable to supplier certificate.
Our 20 vulcanizing presses support daily output of 30,000+ HCR silicone components with Shore A hardness verified on every production batch.
HCR Engineering Capabilities
Three core capability areas where HCR compression molding delivers the highest value for industrial and medical applications.
01
Large-Format Industrial Sealing
HCR compression molding supports component sizes up to 550mm × 550mm — far beyond practical LSR injection limits. Ideal for large industrial enclosure gaskets, heavy-duty sealing mats, and thick-wall vibration isolation pads requiring consistent compression set resistance across millions of duty cycles.
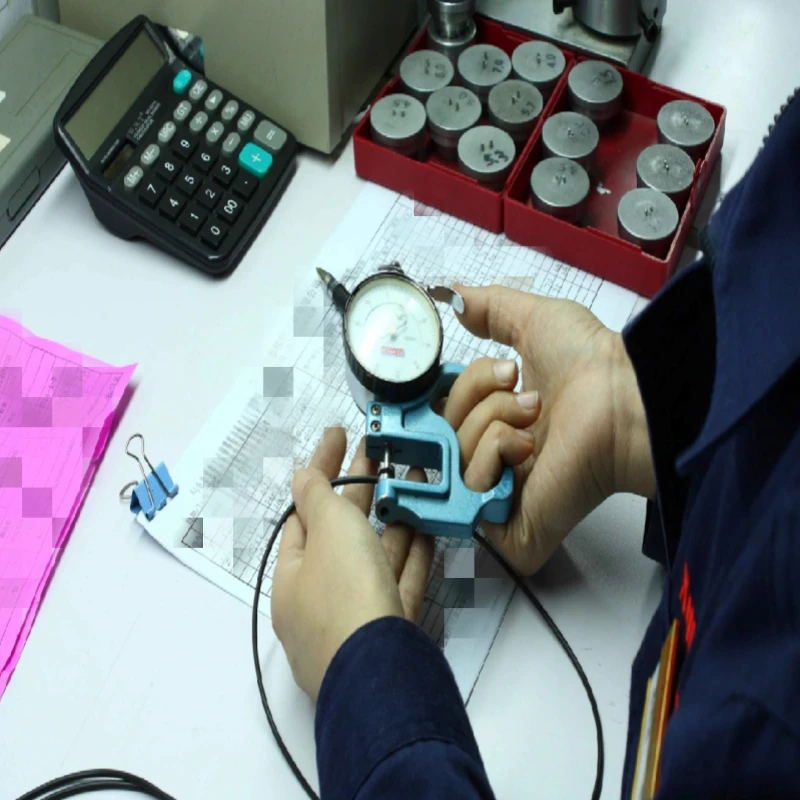
Maximum part size: 550mm × 550mm. Minimum wall thickness: 1mm.
02
Specialized Compound Formulation
HCR compounds support additives incompatible with LSR injection — flame retardant grades meeting UL94-V0, conductive silicone for EMI shielding, and high-tensile strength compounds for dynamic sealing in extreme temperature environments from -60°C to 230°C.
Flame retardant, conductive, and extreme-heat compound formulations available.
03
Medical-Grade HCR Applications
Medical-grade HCR from Elkem, Wacker and Shin-Etsu meets ISO 10993 and USP Class VI requirements. Processed under ISO 13485 quality protocols for large-format medical mats, device sealing interfaces, and applications where LSR injection is cost-prohibitive at required volumes.
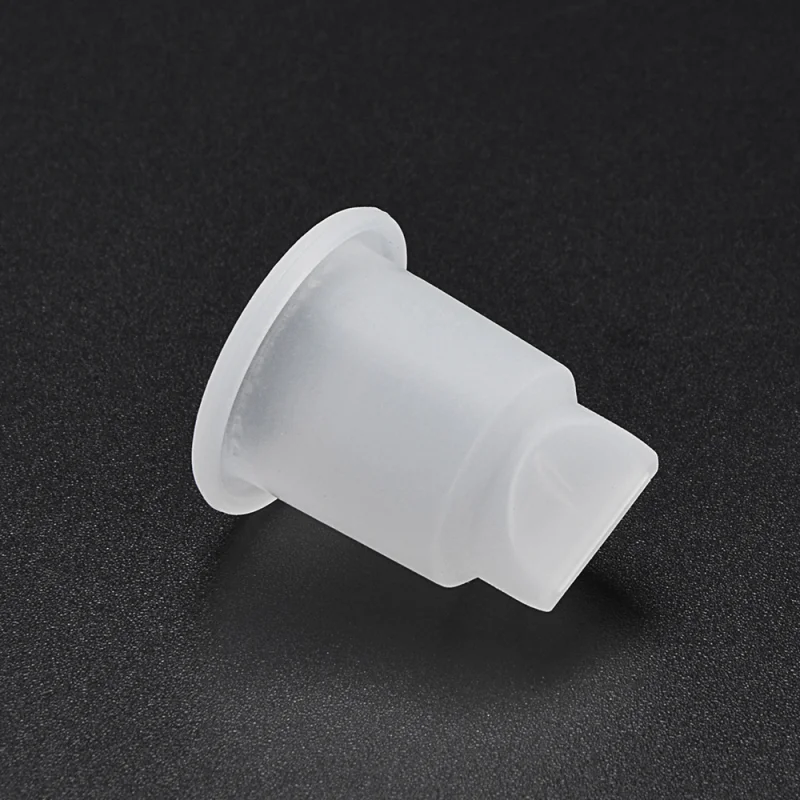
ISO 10993 and USP Class VI compliant HCR compounds processed under ISO 13485 protocols.
Technical Specifications for HCR Silicone
Full process parameters and material compliance data for HCR compression molding programs.
| Parameter | Specification |
|---|---|
| Hardness Range | Shore A 20 – 90 (custom formulations available) |
| Dimensional Tolerance | ISO 3302-1 Class M2 (±0.1mm to ±0.2mm) |
| Maximum Part Size | Up to 550mm × 550mm |
| Wall Thickness Range | 1mm – 50mm+ |
| Operating Temperature | -60°C to 230°C continuous |
| Flame Retardant Grade | UL94-V0 available |
| Material Compliance | FDA 21 CFR / LFGB / ISO 10993 / USP Class VI |
| Raw Material Sources | Elkem/ Wacker / Shin-Etsu / Dow certified compounds |
| Quality Documentation | IRHD hardness report + dimensional OQC per batch |
| T1 Sample Lead Time | 2–3 weeks from drawing approval |
Industries We Serve
HCR compression molding supports applications where large-format geometry, specialized compounds, or cost-efficient tooling are primary requirements.
Frequently Asked Questions for HCR compression
A1:Our facility supports component sizes up to 500mm × 500mm. This covers large industrial enclosure gaskets, medical silicone mats, and thick-wall vibration isolation pads that exceed practical LSR injection size limits.
A2:Yes. We process medical-grade HCR from Wacker, Elkem and Shin-Etsu meeting ISO 10993 and USP Class VI requirements. All medical HCR production is performed under ISO 13485 certified quality management protocols with full material traceability and compliance documentation provided with every batch.
A3:We use precision liquid pigment dosing systems with archived color master samples for every active program. Formulation ratios are locked at first article approval. Color deviation is controlled to within ΔE ≤ 1.5 against the approved master sample for all repeat orders.
A4:Standard HCR compression tooling delivers T1 samples in 2–3 weeks from drawing approval. Complex large-format or multi-cavity tooling may require 3–4 weeks. DFM feedback is provided within 24 hours of receiving your STEP or 2D drawing file.
A5:Choose HCR when your component exceeds 150mm in any dimension, annual volume is below 50,000 pieces, specialized compounds like flame retardant or conductive silicone are required, or initial tooling investment is the primary constraint. For tolerances tighter than ±0.1mm, cleanroom production, or volumes above 100,000 pieces annually, LSR injection is the more suitable process.